Q1. What is a forged steel check valve used for, and where is it used?
A1. A check valve prevents reverse flow and does nothing else — it is not an isolating valve and cannot be used to shut a line down. It is fitted wherever backflow would damage equipment, contaminate a line or drain a header: at the discharge of every pump, on compressor and blower outlets, on the suction of a pump fed from a pressurised source, downstream of a meter, at the outlet of a boiler feed line, and on any branch that must not drain back. It works automatically, with no operator and no external signal, so it has to be chosen so that it neither chatters at low flow nor slams when the flow reverses. Because it is a passive item with no adjustment once it is in the line, its closing behaviour is what decides whether it protects the line or damages it. In forged construction it is used on small-bore high-pressure duty — steam and instrument lines, and services where a sound, radiographically clean body is required.
Q2. What design variants are available, and how do I tell them apart?
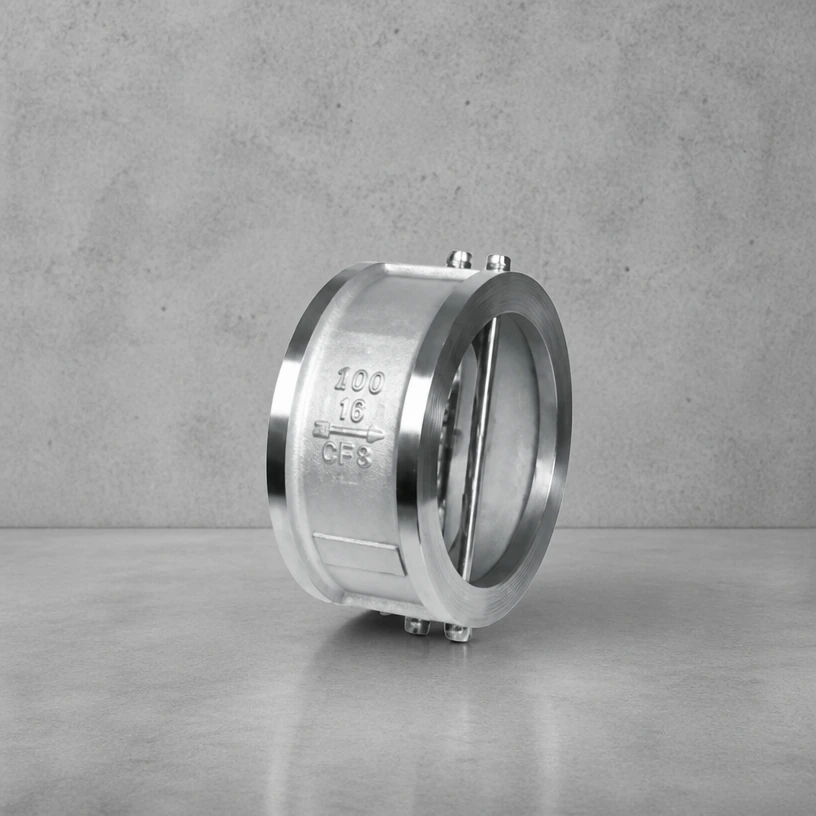
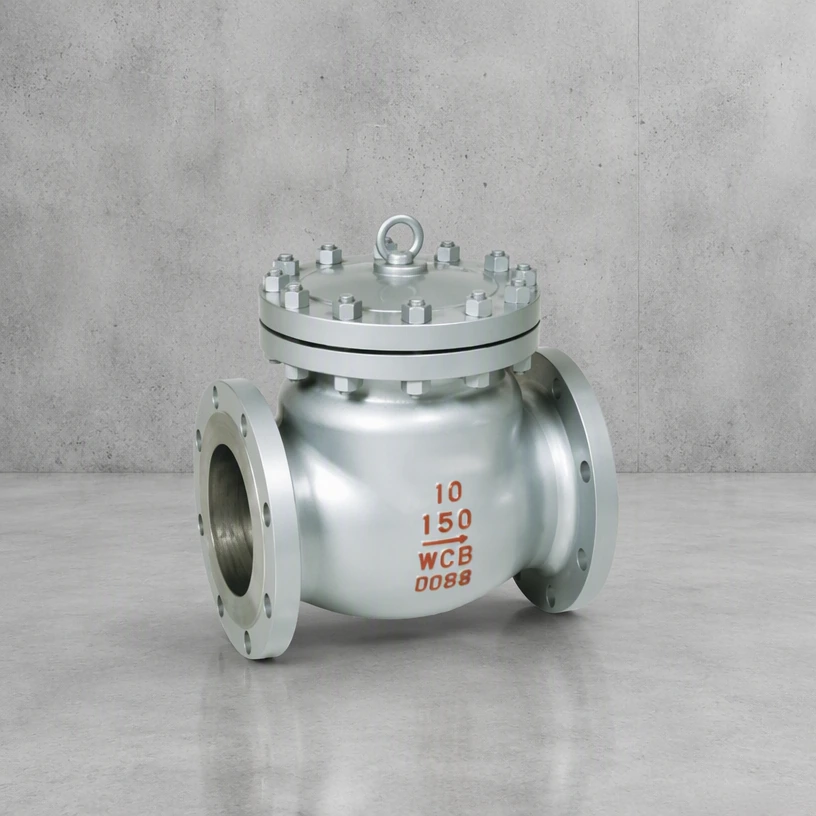
A2. The type is chosen from how much space is available and how fast the flow reverses. A swing check has a hinged disc and is the most common on water and steam mains, but it needs a long installation length and its disc can slam. A dual-plate (wafer) check puts two spring-loaded half discs in a short body, which suits tight spaces and reduces slam. A lift check guides the disc vertically and is used on high-pressure small-bore lines and where the flow is always in one direction. A tilting-disc check is the answer on large compressor and pump discharges, because the disc closes before the flow has fully reversed. Nozzle or axial checks use a spring-loaded ring around the axis and are chosen where the response has to be very fast.
Q3. What is the difference between a forged body and a cast body?
A3. A forged body is formed from solid bar or billet under pressure, so the material is worked and its grain flows around the shape instead of being cast into it. There are no shrinkage cavities or gas pores, and the part can be examined volumetrically — radiographic or ultrasonic — and traced as a single piece of known origin. That is why forged bodies are used on small-bore high-pressure duty — steam and instrument lines, hydrogen and ammonia service, and the higher classes where casting quality is harder to assure in a thick wall. A casting is cheaper and allows a more complex internal shape and a larger bore, and in the common sizes at standard classes the quality is well controlled by the casting standard and by radiographic examination. The working rule is that small and thick-walled goes to forging, large and complex goes to casting.
Q4. How does it compare with the alternative valve types on the same line?
A4. The alternatives worth comparing are the ones that could do the same job at a different cost. A butterfly valve is lighter and cheaper as size grows and needs little space, but its disc sits in the flow and its seat is more easily damaged. A gate valve costs more at small sizes but holds tight more easily and gives an unobstructed bore when open. A ball valve gives quarter-turn operation and is better where the valve is cycled often. A globe valve is chosen only when some regulation is wanted, because it costs permanent pressure drop. A check valve is not an alternative to any of them — it prevents reverse flow and cannot isolate.
Q5. What are the common failure modes, and how are they avoided?
A5. The failures seen in service are fairly consistent, and almost all of them are handling rather than design. Seat damage from particles trapped between the faces, usually caused by using the valve to throttle an abrasive medium. Gland leakage from packing that has aged or a stem that has been scored by over-tightening. Corrosion of the stem and the bonnet bolting where water sits. And seizure after years without operation. The countermeasures are the same in every case: keep the pipework clean before commissioning, work the valve through its full travel periodically, do not leave it part open, and inspect the packing whenever the line is down.
Q6. How do I select the right one for my line?
A6. Two questions decide most of the outcome. The first is what the valve has to do: isolate, regulate, prevent reverse flow or protect against overpressure — the four duties rarely overlap and each points at a different product. The second is what the line can accept in terms of pressure loss, installation length and headroom for the operator. Anything that cannot be answered from the line list should be marked as a question rather than assumed, because the assumptions are what come back as change orders.
Q7. How do I order, and what information is needed for a quotation?
A7. Send the line size, pressure class, medium, working temperature and required connection. Add anything the line demands — sour service, low temperature, a pigging requirement, a control-room signal — and the quotation will come back with the material and seat selection confirmed rather than assumed. Non-standard sizes, alternative operators, trim material and coating can all be produced to order.